If you’re working with two-piece molds—whether you’re a product designer, machinist, or someone testing out new plastic parts—you’ve probably heard the phrase “parting line” get thrown around a lot. But here’s the thing: if you’re dealing with a two-piece mold supplier like me, parting lines aren’t just a technical detail we check off a list. They’re one of the first things we talk about when we get a new project, because get them wrong, and you’re looking at extra costs, part defects, or even a mold that’s unusable. Let’s break down what actually matters when it comes to parting lines in two-piece molds, from someone who’s been doing this long enough to fix a few mistakes I made early on. Two Piece Mold
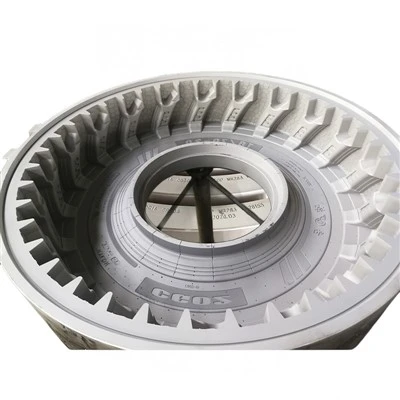
First, let’s keep it simple: a two-piece mold is just two halves—core and cavity, right? The parting line (PL) is where those two halves meet, the thin gap that lets molten plastic flow in and then lets you pull the part out once it cools. Seems basic, but where you put that line makes all the difference. I’ve had a client come to me with a part design they drew up in SolidWorks, and the first thing I’d point out isn’t the mold material or cooling lines—it’s their choice of parting line. They thought it was just a straight line around the part, but no, it’s way more nuanced.
One of the biggest mistakes new folks make is putting the parting line in the wrong place on a part’s surface, especially if there’s any undercut. Wait, what’s an undercut? That’s a part feature that sticks out so it can’t just slide straight out of the mold—like a small hook on the side of a phone case, or a ridge on a toy. If you set your parting line right across that hook, you’re gonna have a bad time. The mold halves won’t close cleanly, and when you try to eject the part, that hook’ll snap right off. Early in my career, I worked on a custom tool for a small appliance maker that had a clip on the inside of their control knob. Their engineer drew the PL straight through the middle of the clip, and we didn’t catch it until we machined both halves. We had to scrap $1,200 worth of tool steel and rework the entire core, just because we didn’t double-check the undercut placement. Now, I make that the first question I ask any new client: “Does your part have any features that would catch on the mold when you open it?” That undercut isn’t a showstopper, but you have to shift the parting line around it so each half of the mold can form that feature cleanly.
Next up, part appearance. Let’s be real—most of the parts we make aren’t hidden inside something else. They’re phone covers, garden tools, kids’ toys that get held up to show off. If your parting line is in a visible spot, that thin seam (called a flash line, even if we try to minimize it) will stick out like a sore thumb. I had a client last year who was making a high-end water bottle lid—they wanted a smooth, seamless look for the brand’s new line. Their original PL was right along the top edge of the lid, where everyone would see it when you set the bottle down. We moved it to the bottom edge, the part that touches the bottle’s surface, where no one would notice it. That small shift made all the difference in their final product, and they’ve been a repeat client ever since. Also, if you’re working with a transparent or colored plastic, like acrylic or ABS, a poorly placed parting line can cause discoloration or streaks. When plastic flows through the gap at the parting line, it can leave a thin ridge that catches light differently, so even a clear part will look like it has a scratch. We’ve started adding a “texture offset” to our parting lines for clear parts—just a tiny adjustment to the angle of the line so the flash is less noticeable, and it’s worked wonders.
Then there’s mold function and how easy (or hard) it is to manufacture. A parting line that’s simple to machine means lower costs and faster turnaround, right? If you pick a super complex, curved parting line that twists around every tiny feature, you’re asking for trouble. Machinists have to mill both halves of the mold to that exact curve, and even a tiny error in the PL will mean the mold doesn’t seal properly. I once worked on a custom tool for a medical component that had a curved ridge all along its length. The client insisted on a parting line that followed that ridge perfectly, but when we machined it, the core and cavity didn’t line up in a few spots—we had to spend an extra three hours hand-polishing the edges to get them to fit. If we’d instead picked a straight parting line that went around the end of the ridge, it would’ve been half the work, and the part would’ve worked just as well. Now, I always push for the simplest possible parting line that meets the part’s needs, because nobody wants to pay for extra machining time.
Another big one: ejection of the part. Once the plastic cools, it shrinks a little and sticks to the core (the side that’s the inner part of the mold). The parting line placement affects how easy it is to push the part out without damaging it. If the parting line is too high on a part with thin walls, the ejection pins might have to push against the side walls, which can warp the part. I learned this the hard way with a small plastic connector—thin walls, only 0.5mm thick, and the client’s PL was right above the pins we needed to use. When we ejected the first test part, the thin walls bent so bad they were unusable. We moved the parting line down to the base of the part, where we could place the pins more evenly around the core, and that fixed the warping immediately. It’s a small adjustment, but it makes a huge difference for parts with delicate features.
Also, don’t forget about material flow. When molten plastic is injected into the mold, it has to flow through the cavity evenly, and the parting line is where the plastic enters the mold (well, usually—gate placement is related, but the PL affects it). If you put the parting line in a spot that creates a dead end for the plastic flow, you’ll get empty spots or uneven cooling in the part. For example, a part with a long, thin shape—like a ruler—will have issues if the PL is on the narrow end, because the plastic has to flow all the way to the other end and might not fill evenly. We usually split the PL down the middle of a part like that, so the plastic flows from both sides and meets in the center. No more gaps, no more uneven plastic density in the final part.
Wait, and let’s talk about flash—you know, that thin excess plastic that oozes out of the mold’s parting line gap. Flash is annoying because it’s extra work to trim off, and too much of it means you have to use more plastic, which adds cost. The parting line’s surface finish matters here, too. If you machine the PL with a smooth, tight gap (usually 0.02mm or less for two-piece molds), you’ll get almost no flash. But if the parting line is angled wrong, even a tiny gap can let plastic seep through. For example, a sharp parting line edge vs. a rounded one—rounded edges reduce the chance of flash forming, because the plastic has less of a sharp edge to catch on. We now add a small radius (0.1mm, usually) to all our parting lines, and our clients have cut their post-mold trimming time by like 20% on average.
I know I’ve been throwing out a lot of technical stuff, but here’s the thing: as a two-piece mold supplier, my job isn’t just to machine a mold. It’s to make sure the part my client makes works, looks good, and doesn’t cost them a fortune. And 9 times out of 10, the parting line is the first thing that makes or breaks that. I’ve had clients come to me thinking they know exactly where the PL should be, and sometimes they’re right, but more often than not, tweaking it a little fixes issues they didn’t even know they’d have—like ejecting a part without breaking it, or getting a smooth surface they can sell to customers.
Let me circle back to that early mistake I made: the appliance knob clip. That cost me and my client time and money, but it taught me to never take a client’s part design at face value. Every time we get a new project, the first step after looking at the part is sitting down with the client to talk through parting line options. We show them 2 or 3 possible PLs, explain the pros and cons of each, and let them pick what works for their part. Some care more about appearance, some care more about cost, some have strict engineering specs they have to follow—we adjust to what they need, not the other way around.
If you’re out there working on a part design, and you’re not sure where to put your parting line, or you’ve tried a PL and you’re having issues with flash, defects, or high costs—hit us up to talk. We’ve worked on everything from tiny medical components to large consumer parts, and we can help you figure out the right parting line for your two-piece mold without the guesswork. No fancy sales pitch, just straight talk about what works, what doesn’t, and how to get a mold that makes great parts.
Special Structure Mold References
- Rosato, D. V., Rosato, M. G., & Rosato, D. V. (2000). Injection Molding Handbook. Kluwer Academic Publishers.
- Todd, R. H., Allen, D. K., & Alting, L. (1994). Manufacturing Processes Reference Guide. Industrial Press Inc.
- Kazmer, D. O. (2007). Injection Mold Design Engineering. Hanser Gardner Publications.
Anhui Varon Mould Co., Ltd.
We are one of the most professional two piece mold manufacturers and suppliers in China, also support customized service. We warmly welcome you to wholesale premium two piece mold made in China here from our factory. If you have any enquiry about cooperation, please feel free to email us.
Address: Anhui Province, Ningguo City, Economic and Technological Development Zone, Heli Industrial Park, Dongcheng Avenue
E-mail: admin@varonmould.com.cn
WebSite: https://www.wanlongmold.com/
